We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Choosing an aluminum scrap melting furnace is a practical decision for recyclers, foundries, and metal processors worldwide. The right furnace affects recovery rate, energy use, melt quality, labor safety, and production consistency. A shiny ingot may look simple, but its quality begins with scrap preparation and furnace control.
Mark E. Schlesinger, author of Aluminum Recycling, has emphasized, “The value of recycled aluminum depends on careful sorting, efficient melting, and controlled processing.” This principle remains useful when comparing furnace designs. Rotary furnaces can handle mixed and contaminated scrap. Reverberatory furnaces suit larger, continuous operations. Induction furnaces offer accurate temperature control and cleaner working conditions. Electric resistance furnaces may help smaller facilities manage installation requirements.
Small details matter. Wet scrap can cause dangerous metal reactions. Excessive oxidation can reduce yield. Poorly designed charging doors may slow production and increase heat loss. These problems are easy to underestimate. I have also seen buyers focus on furnace capacity while overlooking maintenance access, burner efficiency, and local technical support.
This guide reviews seven aluminum scrap melting furnace options for global buyers. Each model should be judged by its real operating environment, not by brochure claims alone. Consider scrap composition, daily throughput, fuel availability, emissions equipment, operator skills, and planned expansion. No furnace is perfect. A technically advanced system may still perform poorly without disciplined sorting and process monitoring. The comparison ahead aims to make that choice clearer, more realistic, and easier to verify.
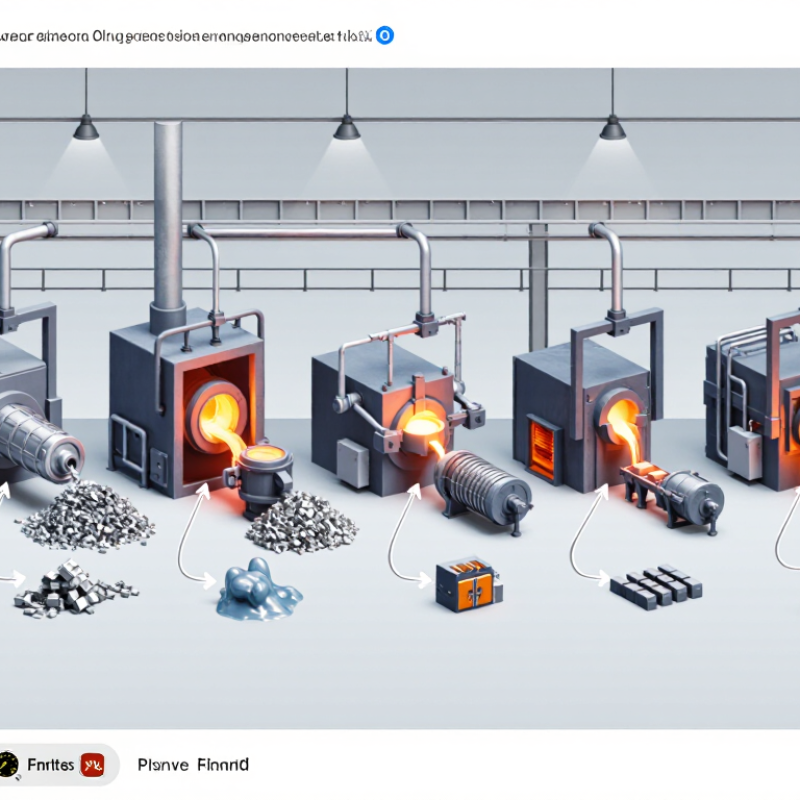
An effective aluminum scrap melting furnace begins with predictable heat transfer. A well-insulated chamber reduces heat loss and shortens melting cycles. Electric resistance, gas, or induction heating can work well when matched to scrap volume and plant utilities. The right choice depends on energy cost, batch size, and local infrastructure.
Furnace design must also handle dirty, mixed scrap. A tilting body helps operators remove metal without excessive manual contact. A dry hearth limits moisture-related hazards and supports safer charging. Mechanical stirring or controlled circulation improves temperature uniformity. This matters when thin sheet, cast parts, and coated offcuts melt together. Reliable temperature sensors are essential. Operators should verify readings with calibrated instruments, because one failed probe can distort an entire batch.
Dross management separates a useful furnace from an expensive one. A suitable skimming system removes oxides while retaining more liquid aluminum. Sealed charging areas and effective exhaust equipment help control smoke and airborne contaminants. Maintenance access matters too. Refractory cracks, worn seals, and blocked burners rarely announce themselves early. In my practical experience, small defects often become large energy losses. No furnace is perfect. A design may perform well but still disappoint when scrap moisture, alloy variation, or operator training changes. Buyers should examine service records, spare-part access, documented safety controls, and measured fuel consumption before choosing among aluminum scrap melting furnaces.
Aluminum scrap rarely arrives in one clean, predictable form. Sorted extrusion and clean sheet usually perform well in reverberatory furnaces, which offer large bath capacity and steady melting. They suit recyclers processing several tonnes daily. However, oxidation losses can rise when operators overheat the surface or hold metal too long.
Induction furnaces provide rapid, controlled melting for clean, dense scrap and smaller batches. Their electromagnetic stirring improves temperature uniformity, but heavily painted or mixed scrap may create slag and unstable operation.
Crucible furnaces remain practical for small workshops and laboratory-scale production. They need less infrastructure, although manual charging can slow output.
Electric resistance furnaces work well for clean charge materials and holding molten aluminum, especially where quiet operation matters.
Rotary furnaces and tilting rotary furnaces handle oily turnings, coated pieces, and less uniform scrap more effectively. Their rotating action exposes the charge to heat, while tilting supports safer metal transfer.
A sidewell furnace can melt clean returns beside a holding chamber, reducing repeated handling. Stack or tower-style furnaces use vertical space and recover heat from exhaust gases, but installation and control can be demanding.
Moisture remains a serious concern. Even a small amount trapped in scrap can cause violent metal reactions.
In practical plant trials, the “best” furnace often changes after testing charge density, salt use, dross rate, energy consumption, and maintenance access.
My early comparisons also underestimated operator training. Equipment alone does not guarantee stable recovery.
Seven Leading Aluminum Scrap Melting Furnace Options Compared
Global buyers usually compare seven furnace types: gas-fired reverberatory, regenerative gas, electric resistance, induction, rotary, tilting, and compact crucible furnaces. Each handles scrap differently. Reverberatory designs suit large batches and steady production. Regenerative models can reduce fuel waste, but their controls are more demanding. Electric resistance furnaces offer clean operation and stable temperature control. They may increase electricity costs in some regions.
Induction furnaces melt quickly and provide strong temperature precision. However, they need reliable power and careful charge preparation. Rotary furnaces handle painted or mixed scrap well, though metal recovery depends on loading practice. Tilting furnaces improve pouring control and reduce manual handling. Compact crucible furnaces fit small workshops, but their capacity may limit future growth. I have seen buyers focus on melting speed first, then discover that maintenance access matters more.
Tips: Compare furnace capacity, energy source, lining life, exhaust treatment, and local service support. Ask for tested recovery data using your actual scrap mix. Check door seals and inspection points. Small details matter.
A practical purchase should also consider alloy separation, operator training, and batch frequency. Temperature records should be easy to review. Safety interlocks are essential. The cheapest furnace is not always economical. A missed maintenance cost can change the entire calculation. Some specifications look impressive on paper, yet real performance depends heavily on scrap moisture, contamination, and loading habits.
7 Best Aluminum Scrap Melting Furnaces for Global Buyers
When comparing seven aluminum scrap melting furnaces, capacity should match your real batch size, not an optimistic sales figure. A furnace rated for 1,000 kilograms may perform poorly with wet, bulky scrap. Check melting time, charge density, holding capacity, and tapping speed. In my experience, reverberatory and rotary furnaces suit larger operations, while crucible, induction, and resistance furnaces often fit smaller batches. Tilting designs can improve pouring control, but they may require more floor space.
Energy use needs practical measurement. Ask for fuel or electricity consumption per ton of aluminum, based on actual scrap conditions. Record startup losses, door opening time, and holding temperature. A lower quoted figure is not always better. Insulation quality, burner adjustment, and operator habits can change results. Safety checks should include lid movement, emergency shutoff, ventilation, molten-metal containment, and moisture control. Even a small amount of trapped water can create a violent reaction.
Tips: Request a test melt with your own scrap. Inspect refractory wear after repeated cycles. Check whether heating elements, burners, thermocouples, and filters are locally available. Maintenance should be simple enough for trained technicians to complete safely. Keep service records. I would also leave space for future repairs; compact layouts often look efficient but become frustrating later. Mistakes happen. A careful inspection prevents expensive surprises.
| Rank | Furnace Type | Typical Melting Capacity | Typical Energy Use* | Best Scrap Applications | Temperature Control | Safety Profile | Maintenance Demand | Main Advantages | Key Limitations | Recommended Buyer Profile |
|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Regenerative Gas-Fired Reverberatory Furnace | 5–20 tonnes/hour 30–100 tonnes/day | 650–900 kWh equivalent/tonne of molten aluminum | High-volume, pre-sorted aluminum scrap, sheet, extrusion, and castings | Good; automated burner and bath-temperature control are commonly available | High Requires combustion-gas monitoring, burner interlocks, ventilation, and molten-metal spill protection | Medium Burners, refractory lining, doors, seals, and recuperation equipment require scheduled inspection | High throughput, lower fuel consumption than conventional gas systems, suitable for continuous production | Large footprint; metal oxidation and dross formation can increase with excessive turbulence or long holding times | Large secondary aluminum plants and continuous foundry operations |
| 2 | Electric Induction Furnace | 0.5–10 tonnes/hour | 600–800 kWh/tonne of molten aluminum | Clean, dense scrap, remelt ingot, runners, returns, and controlled alloy batches | Very good; rapid power adjustment and accurate bath monitoring are possible | High Requires water-cooling protection, electrical interlocks, grounding, and strict moisture control | Medium Coil, refractory lining, cooling system, and power electronics need regular checks | Fast melting, precise control, no direct combustion emissions at the furnace, and flexible batch operation | Unsuitable for heavily contaminated or highly oxidized scrap without suitable pretreatment; electricity supply must be reliable | Medium-sized foundries, alloy producers, and facilities requiring frequent alloy changes |
| 3 | Gas-Fired Rotary Furnace | 1–10 tonnes/batch 1–5 batches/hour | 700–1,000 kWh equivalent/tonne of molten aluminum | Mixed, thin, coated, oily, or contaminated scrap with a high surface-area-to-weight ratio | Good; controlled rotation and burner adjustment support uniform heating | Medium–High Requires robust charging procedures, gas safety systems, fume extraction, and splash protection | Medium–High Rotary seals, refractory lining, drive components, and burner systems experience substantial wear | Handles difficult scrap, improves metal recovery compared with simple open melting, and supports flexible batch sizes | Higher refractory and mechanical wear; dross and oxide management remain important | Recycling plants processing variable-quality or contaminated aluminum scrap |
| 4 | Electric Resistance Crucible Furnace | 50–1,000 kg/batch | 700–1,000 kWh/tonne of molten aluminum | Clean returns, ingot, small castings, and low-to-medium volume production | Good; digital controllers can maintain stable holding and melting temperatures | High Lower combustion exposure, but operators still need protection from molten metal and electrical hazards | Low–Medium Heating elements, thermocouples, crucible condition, and insulation require routine inspection | Simple operation, clean working environment, compact installation, and relatively low initial complexity | Limited batch size and slower melting for large scrap pieces or high-throughput applications | Small foundries, laboratories, maintenance shops, and low-volume casting operations |
| 5 | Gas-Fired Crucible Furnace | 50–1,500 kg/batch | 900–1,200 kWh equivalent/tonne of molten aluminum | Clean ingot, returns, and small quantities of sorted scrap | Moderate; temperature stability depends on burner control and operator practice | Medium Needs flame-failure protection, gas-leak detection, ventilation, and safe crucible handling | Low–Medium Crucible, burner, refractory, thermocouple, and gas train need periodic service | Low purchase cost, straightforward installation, and useful where electricity capacity is limited | Higher fuel consumption and heat loss; less suitable for dirty scrap or continuous high-volume production | Small and medium foundries in regions with accessible, economical gas supplies |
| 6 | Tower or Shaft Melting Furnace | 2–15 tonnes/hour | 550–750 kWh equivalent/tonne of molten aluminum | Consistent, compacted, and pre-sorted scrap with stable feed composition | Good; controlled charging and melting zones provide stable operation | Medium–High Requires controlled charging, dust and fume extraction, interlocks, and reliable feed equipment | Medium–High Charging mechanisms, refractory zones, burners, and filters need planned maintenance | High thermal efficiency, compact footprint for its output, and low energy use with suitable feedstock | Performance drops with wet, bulky, highly contaminated, or irregularly sized scrap; pretreatment is often essential | Large recycling operations with reliable scrap sorting and compacting systems |
| 7 | Electric Sidewell or Holding Furnace with Charging Well | 1–8 tonnes/hour 5–30 tonnes holding capacity | 600–850 kWh/tonne of molten aluminum | Continuous casting, die casting, and operations using preheated or prepared scrap and returns | Very good; separate melting, holding, and transfer zones help stabilize alloy temperature | High Requires level controls, electrical protection, dry charging, and safe molten-metal transfer procedures | Medium Pumps, refractory, heating elements, thermocouples, and transfer channels require inspection | Stable metal delivery, low temperature variation, reduced holding losses, and good compatibility with automated lines | Higher installation complexity; generally needs prepared feedstock and integration with downstream equipment | Automated casting lines and plants requiring continuous, tightly controlled molten aluminum supply |
*Energy figures are typical engineering ranges for melting aluminum to approximately 700–760°C under suitable operating conditions. Actual consumption varies with scrap cleanliness, moisture, charge density, furnace size, insulation, burner or power-system efficiency, holding time, and local fuel or electricity conditions. All aluminum scrap should be dry, properly sorted, and free from sealed containers before charging.
Global buyers should evaluate furnaces against scrap quality, power supply, and production rhythm. Aluminum scrap often carries paint, oil, moisture, and mixed alloys. These contaminants affect melt loss, dross formation, and worker safety. The International Aluminium Institute reports that recycling aluminum uses about 5% of the energy required for primary production. That advantage disappears when a furnace has poor insulation, unstable temperature control, or excessive holding time.
Capacity should match the real batch size, not the supplier’s maximum figure. Compare melting rate, fuel consumption, refractory life, and recovery percentage under similar scrap conditions. Gas-fired, electric resistance, induction, and rotary designs each suit different operating environments. Electric systems may fit regions with reliable low-carbon power. Fuel-fired systems may offer simpler installation where electricity is expensive. Ask for measured data, not attractive estimates. The U.S. Department of Energy identifies process heating as a major industrial energy-use area, so small efficiency losses can become large annual costs.
Check loading access, fume extraction, slag removal, spare-part availability, and local technical support. A furnace should also provide accurate thermocouples and simple controls. Over-automation can create repair delays in remote plants. No furnace is perfect. Buyers should request references from facilities processing similar scrap, then inspect maintenance records and actual fuel or electricity bills. The best choice is rarely the largest model; it is the one that remains stable during dirty, uneven, and changing scrap loads.
We use cookies on our website to give you an improved browser experience. View our Privacy Policy for more information. Please make your selection to opt in or out of ALL cookies here: Accept or Decline
Do you consent to the use of ALL cookies?
901 2nd Court West
Birmingham, AL 35204
Sales: 866.481.4036
Logistics/Ops: 866.481.4036
2101 Dralle Road
University Park, IL 60466
Sales: 708.813.9070
Logistics/Ops: 708.235.4200
400 E. 13th Street
Little Rock, AR 72114
Sales: 866.760.5344
Logistics/Ops: 866.760.5344
225 Collins Road
Elkhart, IN 46515
Sales: 574.295.0214
Logistics/Ops: 574.607.4611
601 Berryman Pike
Tipton, IN 46072
Sales: 800.897.7591
Logistics/Ops: 800.897.7591
3900 Uvalda Street
Denver, CO 80239
Sales: 303.706.8000
Ops/Logistics: 303.576.8398
510 3rd Street E
Milan, IL 61264
Sales: 800.322.1052
Logistics/Ops: 800.322.1052
1660 E. Aurora
Des Moines, IA 50313
Sales: 800.671.1660
Logistics: 800.671.1660
86554 Gene Lasserre Blvd.
Yulee, FL 32097
Sales: 904.253.3060
Logistics/Ops: 904.225.3000
694 S.E. County Road 245
Lake City, FL 32025
Sales: 800.727.6706
Logistics/Ops: 386.752.7412
210 Neptune Road
Auburndale, FL 33823
Sales: 863.967.1131
Logistics/Ops: 863.777.9814
4601 McCoy Drive
Pensacola, FL 32503
Sales: 850.308.7030
Logistics/Ops: 850.434.5502
815 South 56th Street
Tampa, FL 33619
Sales: 813.302.1940
Logistics/Ops: 813.621.1352
200 Hosea Road
Lawrenceville, GA 30046
Sales: 770.953.7575
Logistics/Ops: 770.513.6000
Branch Product Guide
Branch Line Card
Moulding Offering
Cedar Offering
Column Offering
8173 Hwy. 165 North
Monroe, LA 71211
Sales: 800.256.4165
Logistics/Ops: 800.256.4165
508 Warren Avenue
Portland, ME 04103
Sales: 207.888.2331
Logistics/Ops: 207.797.6565
4300 Georgia Pacific Blvd.
Frederick, MD 21704
Sales: 301.798.7474
Logistics/Ops: 301.874.8000
419 Maple Street
Bellingham, MA 02019
Sales: 508.449.0535
Logistics/Ops: 508.966.5500
825 Buchanan Ave SW
Grand Rapids, MI 49507
Sales: 877.800.1180
Logistics/Ops: 616.278.0909
995 Pacific St. NW
Aitkin, MN 56431
Sales: 800.432.3727
Logistics/Ops: 218.212.7770
1102 Port Terminal Drive
Duluth, MN 55802
Sales: 800.951.9899
Logistics/Ops: 800.851.9899
9110 83rd Ave. North
Brooklyn Park, MN 55445
Sales: 763.425.0204
Logistics/Ops: 763.425.0204
910 E. Railroad Street
Long Beach, MS 39560
Sales: 866.535.4135
Logistics/Ops: 228.205.2400
1727 Warren Street
North Kansas City, MO 64116
Sales: 800.621.2611
Logistics/Ops: 800.621.2611
2123 North Golden
Springfield, MO 65803
Sales: 800.375.7891
Logistics/Ops: 800.375.7891
13860 Corp. Woods Trail
Bridgeton, MO 63044
Sales: 314.209.0800
Logistics/Ops: 314.209.0800
1109 South 19th Street
Omaha, NE 68108
Sales: 800.489.6637
Logistics/Ops: 800.489.6637
1 Luger Road
Denville, NJ 07834
Sales: 973-339-3539
Logistics/Ops: 973.625.1461
3720 Jeffrey Blvd.
Blasdell, NY 14219
Sales: 716.235.5989
Logistics/Ops: 716.825.6557
319 Yaphank Ave.
Yaphank, NY 11980
Sales: 631.358.5714
Logistics/Ops: 631.924.7401
3300 Parkside Drive
Charlotte, NC 28208
Sales: 800.839.2588
Logistics/Ops: 704.394.3172
1712 East D Street
Butner, NC 27509
Sales: 984.389.8200
Logistics/Ops: 919.575.3700
128 Foothills Drive
Statesville, NC 28687
Sales: 800.222.1414
Logistics/Ops: 704.394.3172
550 Munroe Falls Rd.
Tallmadge, OH 44278
Sales: 330.357.4506
Logistics/Ops: 330.794.1141
10347 Toebben Dr.
Independence, KY 41051
Sales: 859.298.3926
Logistics/Ops: 859.746.2250
450 N. MacArthur
Oklahoma City, OK 73127
Sales: 800.375.6025
Logistics/Ops: 800.375.6025
1680 North Aspen
Broken Arrow, OK 74012
Sales: 918.272.2212
Logistics/Ops: 918.272.2212
522 Bridge Street
Hunker, PA 15639
Sales: 878.217.2001
Logistics/Ops: 724.925.7285
4290 Atlanta Street
Charleston, SC 29418
Sales: 843.371.1420
Logistics/Ops: 843.554.8192
1040 S. Industrial Dr.
Erwin, TN 37650
Sales: 423.641.1005
Logistics/Ops: 423.742.5911
4287 Pilot Drive
Memphis, TN 38118
Sales: 901.365.2101
Logistics/Ops: 901.365.2101
700 Myatt Drive
Madison, TN 37115
Sales: 615.327.9547
Logistics/Ops: 629.777.4949
4747 Mark IV Parkway
Fort Worth, TX 76106
Sales: 866.323.5117
Logistics/Ops: 817.625.9091
6990 Market Avenue
El Paso, TX 79915
Sales: 915.778.6356
Logistics/Ops: 915.265.7200
2502 Wilson Road
Harlingen, TX 78552
Sales: 800.580.6711
Logistics/Ops: 800.580.6711
10,000 North Loop East
Houston, TX 77029
Sales: 713.921.1977
Logistics/Ops: 713.675.3544
702 East 44th St.
Lubbock, TX 79404
Sales: 866.454.6010
Logistics/Ops: 866.454.6010
535 N. WW White Road
San Antonio, TX 78219
Sales: 800.284.0488
Logistics/Ops: 210.333.8112
142 Pine Haven Shores Rd.
Shelburne, VT 05482
Sales: 802.800.2540
Logistics/Ops: 802.985.2512
4700 Bethlehem Road,
Richmond, VA 23230
Sales: 804.201.2400
Logistics/Ops: 804.342.1161
4516 N Barker Road
Spokane Valley, WA 99027
Phone: 509.892.9420
Toll free: 800.728.6157
8365 N. 76th Street
Milwaukee, WI 53223
Sales: 800.356.9245
Logistics/Ops: 800.356.9245
312 S. Chester Street
Sparta, WI 54656
Sales: 800.362.5864
Logistics/Ops: 800.362.5864
899 Grossman Drive
Schofield, WI 54476
Sales: 800.472.0017
Logistics/Ops: 800.472.0017
